
Modern metalworking requires processes that combine high dimensional accuracy with economical production speeds. This is why thermal cutting has become established in many industrial sectors. Technological developments in fibre and CO₂ lasers have expanded the processing of materials and now make intricate geometries possible. Stainless steel places particular demands on the process, because the material, sheet thickness, laser power, cutting gas and process parameters must be matched to one another. In industrial practice, this coordination has a significant influence on cut quality, the heat-affected zone and the required rework effort.
Process principle and physical fundamentals of laser cutting
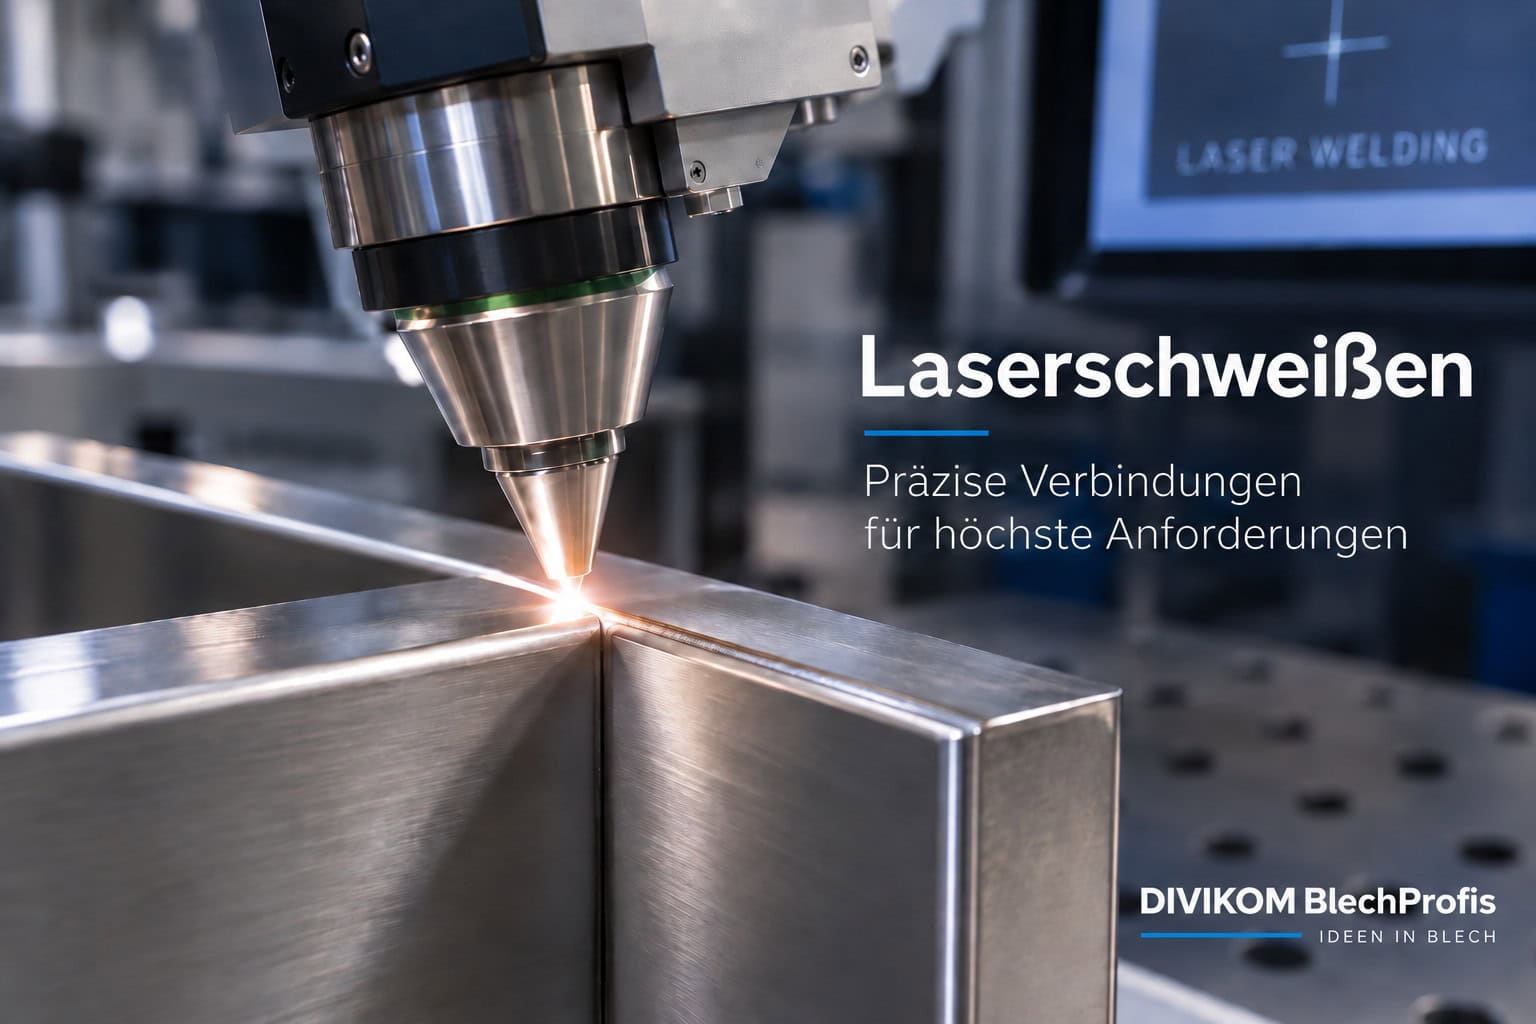
The thermal cutting process is based on the targeted concentration of light energy onto a small area of the workpiece. In laser fusion cutting stainless steel is heated locally above its melting temperature. A directed gas jet then removes the molten material from the kerf. This basic process principle describes Fraunhofer IWS.
The high gas pressure creates a characteristic striation pattern. At the same time, the heat-affected zone remains comparatively small. inert gas can also reduce oxide formation on the cut edge. Argon and nitrogen are used in particular for stainless steel, as these gases do not react with the molten metal. This makes it possible to produce cut edges with low oxidation.
In addition to fusion cutting, there are other variants of laser cutting. However, for stainless steel, fusion cutting with a suitable inert gas is the focus. The actual cut quality depends on several influencing factors. These include, among others, material thickness, alloy, laser power, gas pressure, focus position and feed rate. A general assessment is therefore only possible to a limited extent.
Material thicknesses, kerf widths and technological limits
The performance of modern laser systems is particularly evident when processing different sheet thicknesses. TRUMPF generally describes laser cutting for sheet thicknesses from 0.5 mm to over 30 mm. The stainless steel thickness that can actually be achieved, however, depends on the respective system, the laser power and the process parameters used (Technology comparison: laser cutting). The stated figure is therefore not to be understood as a universal performance limit for every stainless steel system.
As material thickness increases, cutting efficiency generally decreases. A Fraunhofer study explains this trend by the fact that at lower cutting speeds more heat is conducted away into the material (Fraunhofer study on cutting efficiency). At the same time, the requirements for matching laser power, cutting gas and feed increase.
A key advantage of the technology lies in the narrow kerf. TRUMPF states a kerf of less than 0.5 mm for laser cutting. This makes small internal contours and intricate geometries possible. The specific outcome, however, also depends on the material, sheet thickness, contour and system configuration.
If the parameters are unsuitable, incomplete cuts, a pronounced striation pattern or burr on the underside can occur. Compared with plasma and flame cutting, laser cutting is said to produce low edge roughness, little burr and little dross. The need for rework, however, depends on the respective sheet thickness and process conditions.
Cutting gases and cut-edge quality
The choice of assist gas influences the cut edge and the course of the cutting process. When cutting stainless steel, nitrogen or argon are often used. Both gases do not react with the molten metal and are therefore suitable for cut edges with low oxidation (TRUMPF on cutting gases). The gas jet also assists in expelling the melt from the kerf.
A high gas pressure helps remove the melt and creates the characteristic striation pattern typical of the process. Depending on the settings and material thickness, the cut edge can therefore exhibit different surface characteristics. The quality should therefore not be assessed solely on the basis of the gas used. What matters is the interaction of gas type, pressure, laser power, focal position and cutting speed.
In industrial manufacturing, the remaining burr on the underside of the component is assessed carefully. Studies by Fraunhofer IWS show that adhering burr on laser-cut stainless steel of alloy 1.4301 can act as a crack initiator. In the tests described, removing the burr increased the permissible fatigue strength by about 10 % (Fraunhofer IWS annual report). For components subjected to cyclic loading, inspection and, if necessary, post-processing of the cut edge can therefore be useful.

Plant and process types in modern production
Different beam sources and machine concepts are used in laser cutting systems. A Fraunhofer study on cutting efficiency shows that fibre lasers can achieve higher cutting efficiency than CO₂ lasers for thin sheet metal. However, according to this study, their efficiency drops more quickly as material thickness increases (Fraunhofer study on cutting efficiency). The results describe fundamental efficiency trends and do not provide a universal cutting speed for every stainless steel grade and every system.
In addition to classic two-dimensional laser cutting, there are processes for special geometries. For laser remote cutting, a higher speed and generally a smaller heat-affected zone than with classic laser cutting have been described (Fraunhofer IWS on laser remote cutting). Whether this process is suitable depends on the component, contour and system concept.
For industrial practice, adapting the machine to the specific task is also of central importance. Thin sheet metal, large outer contours, small internal cut-outs and complex geometries each place different demands on beam guidance, motion system, gas supply and process control. The properties of a particular laser type therefore cannot simply be transferred to every application.
Economic aspects and areas of application
The economical operation of a laser cutting system depends on several factors. These include, among others, utilisation, material thickness, cutting speed, gas consumption, scrap, and the effort required for post-processing. For stainless steel, it is also necessary to consider that profitability is strongly influenced by alloy, geometry and the required edge quality.
Careful nesting of contours can reduce material usage. At the same time, the arrangement of the components must be chosen so that thermal load and processing time remain manageable. Laser cutting is particularly suitable for tasks where small internal contours, delicate geometries and reproducible cut edges are required. However, the specific suitability must be checked against the component requirements and the available machine technology.
After the actual separating process, further steps in the production chain may be required. These include, for example, removing a burr, inspecting the cut edge or subsequent forming. The necessary effort depends on the sheet thickness, the cutting quality and the later loading of the component.
Material thickness also influences productivity. As cutting efficiency generally decreases as thickness increases, process design for thicker sheet must be carried out particularly carefully. Statements on speed, maximum thickness and cost-effectiveness are therefore always dependent on the equipment, laser, gas, alloy and geometry.
Future prospects for thermal cutting
Further development of laser cutting is focused on better coordination of the beam source, cutting head, gas supply and process control. The aim is to keep cut quality stable and to manage energy and gas consumption appropriately. Automated monitoring systems can help detect process deviations and make production more repeatable.
Another prospect lies in processes that combine high processing speeds with a small heat-affected zone. Laser remote cutting has been described in this context as a productive variant. However, its suitability still depends on component shape, material and system concept.
Laser cutting stainless steel therefore remains a versatile thermal cutting process. Its advantages lie in the narrow kerf, the ability to produce fine contours and the comparatively small heat-affected zone. At the same time, material thickness, cutting gas and edge requirements require careful process design.
What is meant by laser cutting stainless steel?
Laser cutting stainless steel is a thermal cutting process in which the metal is heated locally above its melting point. A directed gas jet removes the molten material from the kerf. When argon or nitrogen is used, cut edges with low oxidation can be produced.
What role does nitrogen play in cutting stainless steel?
Nitrogen serves as an inert gas in fusion cutting. It does not react with the molten metal and can therefore reduce oxide formation on the cut edge. In addition, the gas jet helps expel the melt from the kerf.
What material thicknesses can be processed with the laser?
TRUMPF generally describes laser cutting for sheet thicknesses from 0.5 mm to over 30 mm. However, the stainless steel thickness that can actually be achieved depends on the system, laser power, material, cutting gas and process parameters. The general manufacturer specification therefore cannot be transferred to every machine.
Why is the heat-affected zone so small during laser cutting?
The laser energy is concentrated on a small area. In laser fusion cutting, this means that only a limited zone of the material is melted. According to Fraunhofer IWS, a high gas pressure results in a small heat-affected zone. However, its actual size depends on the respective process conditions.
Which downstream working steps are often required?
Depending on sheet thickness and process control, a burr may remain on the cut edge. This can be particularly relevant for components subject to cyclic loading and may need to be removed. Further working steps depend on the component geometry, the required edge quality and the subsequent production process.
A coordinated process chain runs from the digital geometry and nesting of the contours to inspection and possible post-processing of the finished sheet metal part. The precise interaction of material, laser system, cutting gas and process parameters determines whether the required cut quality can be achieved economically. This is why laser cutting stainless steel remains an important process for precise and flexible sheet metal fabrication.
 German
 English